Top Custom Vacuum Conveying Systems from Trusted Suppliers - Quality You Can Rely On
Experience unparalleled reliability with our Vacuum Conveying Systems, expertly designed to meet the unique demands of diverse industries. With years of specialization, we deliver high-performance solutions that ensure efficient and safe material transfer. At Jiangsu Kelong Machinery Co., Ltd., we take pride in our ability to provide customized approaches tailored to your operational needs. Our systems focus on minimizing downtime and boosting productivity, offering exceptional returns on your investment.

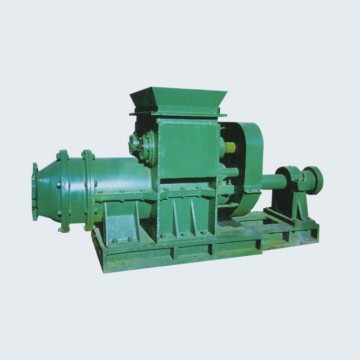
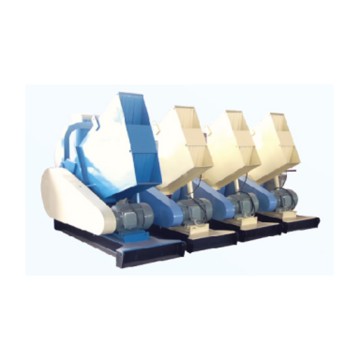
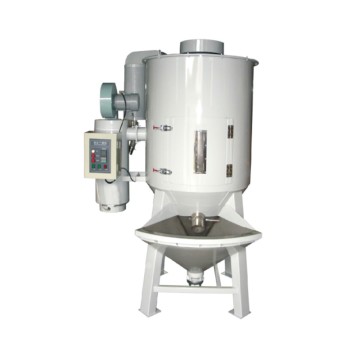
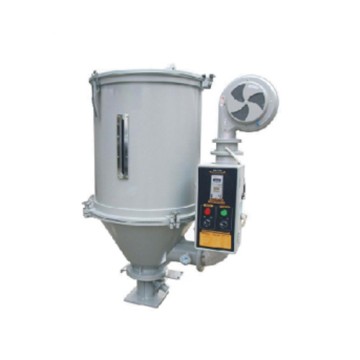
How To find Vacuum Conveying System Delivers Unmatched Quality Application
In the ever-evolving landscape of manufacturing, ensuring high-quality output while maximizing efficiency is a fundamental challenge. One innovative solution to this challenge is the vacuum conveying system, a technology designed to streamline the movement of bulk materials with precision and care. Notably, vacuum conveying systems prevent contamination and degradation of sensitive materials, making them indispensable in applications where quality is paramount. By utilizing controlled environments that minimize exposure to external factors, these systems help maintain the integrity of materials from storage to processing.
The implementation of a vacuum conveying system can transform operations across various industries, from construction to pharmaceuticals. These systems not only enhance productivity but also reduce labor costs and material waste. By automating the transfer process, businesses can achieve consistent product quality and maintain rigorous compliance with industry standards. Furthermore, the adaptability of vacuum conveying solutions ensures compatibility with a wide range of materials, making them a versatile choice for manufacturers focused on optimizing production while safeguarding quality.
Choosing the right vacuum conveying system is critical for achieving unmatched quality in application. It is essential for buyers to consider factors such as material characteristics, production capacity, and integration capabilities with existing processes. Collaborating with experienced manufacturers who understand industry's nuances can lead to tailored solutions that meet specific operational needs. This strategic approach not only enhances productivity but also fortifies the overall quality assurance framework, fostering long-term success in today's competitive market.
How To Find Vacuum Conveying System Delivers Unmatched Quality Application
| Application Area | Material Type | System Efficiency (%) | Maintenance Frequency (Months) | Dust Control Features |
|---|---|---|---|---|
| Food Processing | Powder & Granules | 95 | 6 | Integrated Filter System |
| Pharmaceutical | Powders | 98 | 4 | HEPA Filtration |
| Plastic Industry | Resins & Pellets | 90 | 12 | Cyclone Separator |
| Mineral Processing | Fine Powders | 92 | 8 | Dust Suppression System |
| Chemical Industry | Powder & Liquid | 94 | 5 | Ventilation System |
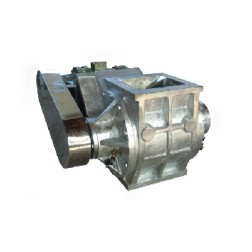
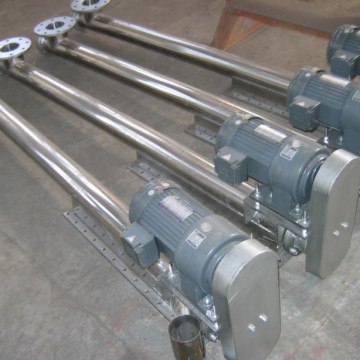
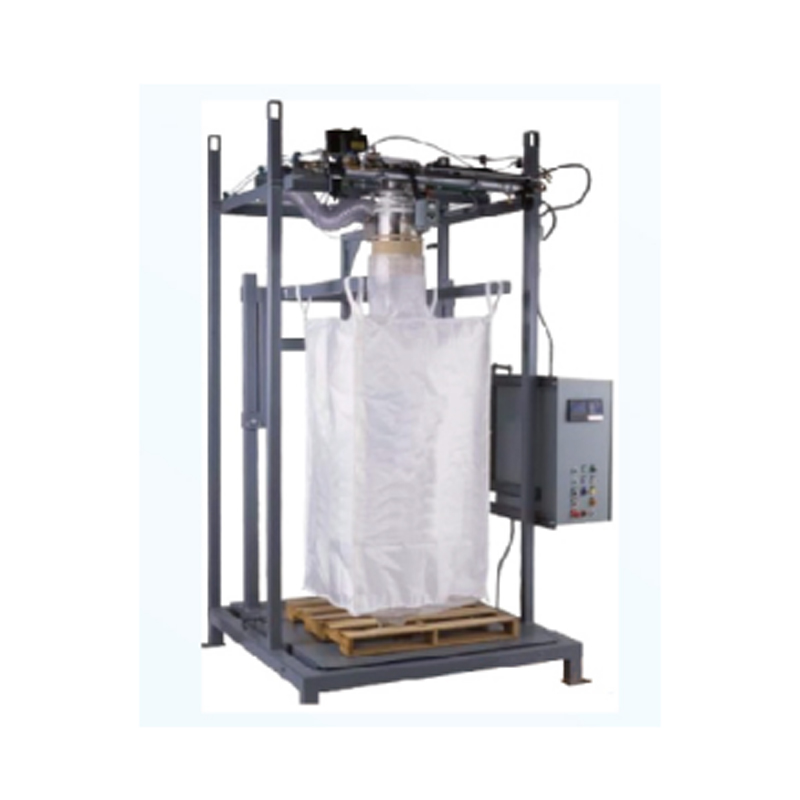
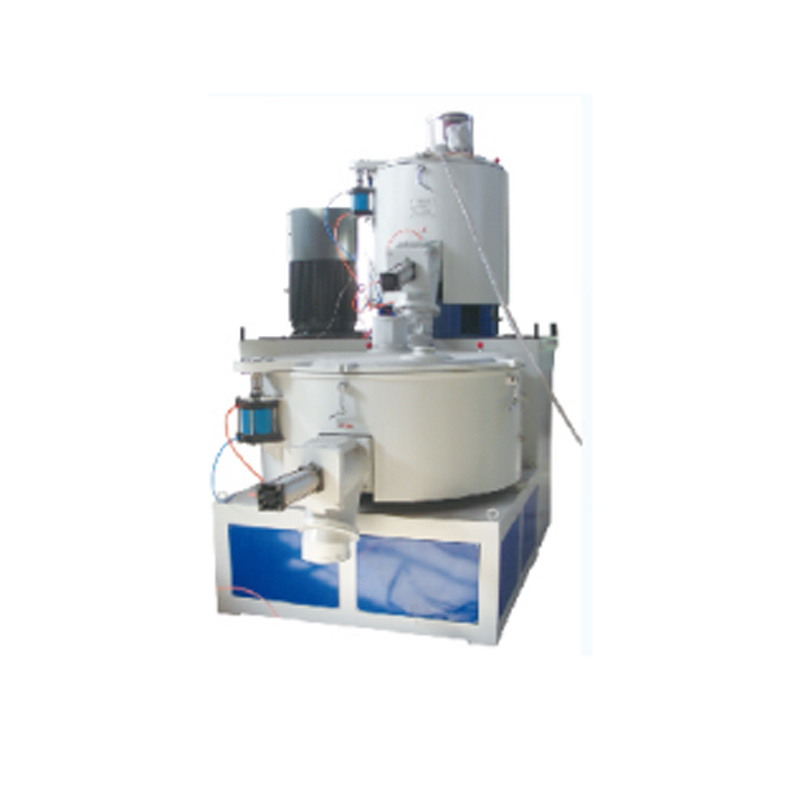
Quick Tips To Vacuum Conveying System Where Service Meets Innovation Factory-Direct Excellence
L
Linda Clarke
I highly recommend this product! The durability is great, and the customer support staff are incredibly knowledgeable and professional.
14
August
2025
I
Isabella Thomas
Great quality! I was pleasantly surprised by the knowledgeable support team, who helped me every step of the way.
14
August
2025
D
Daniel Harris
Quality and reliability at its best. After purchasing, I felt well-supported by a truly professional team.
08
August
2025
D
Daniel King
Superb quality! The professionalism of the after-sales team really stood out during my experience.
15
August
2025
E
Ethan Hill
Quality and service went beyond my expectations. The representatives were friendly and highly knowledgeable.
21
August
2025
M
Mila Lee
The product is exactly what I needed! The service team’s expertise and enthusiasm made all the difference.
13
August
2025